Pneumatic Ball Valve About
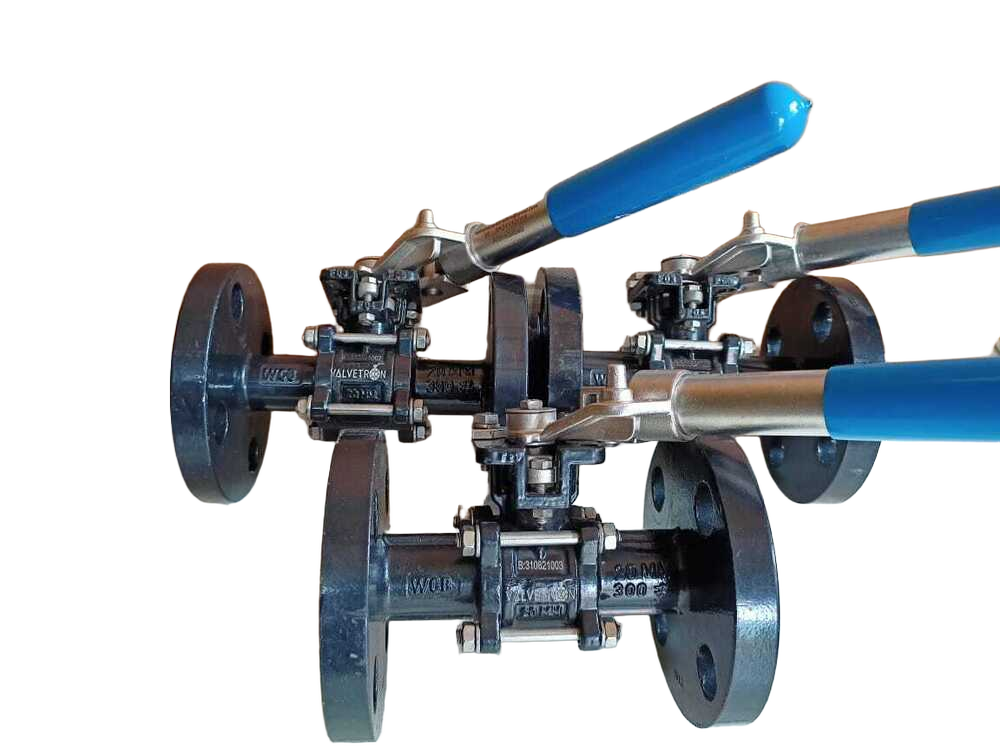
Unlock instant savings with our new Pneumatic Ball Valve, engineered for commanding performance in demanding industrial settings. This unmatchable valve features a rack and pinion pneumatic actuator with a mechanical position indicator on top, ensuring precise control in every cycle. Its robust epoxy-coated body withstands corrosion, while the versatile design meets ANSI, DIN, and JIS standards. With up to 100,000 cycles, Class VI bubble-tight sealing, and a gorgeous ISO 5211 mounting pad, this valve elevates automation across water, chemical, oil & gas, and fluid control systems.
Unmatched Versatility for Industrial Applications
This Pneumatic Ball Valve is used for precise flow regulation in fluid control systems, chemical processing plants, water treatment facilities, and oil & gas pipelines. Featuring a double acting or spring return actuator, sturdy stainless steel or alloy body, and visual position indicator, it offers flexible configuration and reliable performance. Its compact mounting and floating ball design make it compatible for tight spaces, while robust sealing ensures bubble-tight closure for air, water, gas, oil, steam, and chemical applications.
Convenient Order Processing & Secure Packaging
Enjoy streamlined order processing and lowest price assurance for every valve purchase. Sample units are available on request for quality reference. Each Pneumatic Ball Valve is carefully packed in sturdy, industry-standard cartons or crates, ensuring safe arrival during dispatch to your location. With timely packing & dispatch, customers receive products in pristine condition, ready for immediate installation on-site. Flexible payment terms cater to diverse procurement requirements, simplifying your sourcing experience from manufacturer or supplier in India.
FAQ's of Pneumatic Ball Valve:
Q: How does the rack and pinion pneumatic actuator enhance valve performance?
A: The rack and pinion pneumatic actuator delivers efficient, reliable torque for both on/off and modulating control, ensuring rapid and precise valve operation, even in demanding industrial environments.
Q: What are the site applications of this Pneumatic Ball Valve?
A: This valve is ideal for industrial automation, fluid control systems, chemical processing plants, water treatment facilities, and oil & gas pipelines, providing robust flow management across multiple sectors.
Q: When should you opt for a Class VI bubble-tight leakage rating?
A: Choose the Class VI bubble-tight rating when applications require zero leakage for safety, environmental compliance, or precise regulation-such as in chemicals, steam, or gas lines.
Q: Where can the product be installed considering end connection options?
A: Thanks to ANSI, DIN, and JIS standard compatibility, along with flanged, threaded, or welded ends, these valves can be installed in a wide range of international industrial setups.
Q: What benefits come with the epoxy powder-coated body?
A: The epoxy powder coating provides excellent corrosion resistance, extending the valve's lifespan in harsh environments and reducing maintenance costs over time.
Q: How is the product packaged and dispatched for safe delivery?
A: Each unit is packed in durable cartons or crates, ensuring protection during transport. Packing & Dispatch processes are meticulously managed to deliver products safely and promptly to your location.


 Send Inquiry




 Send Inquiry